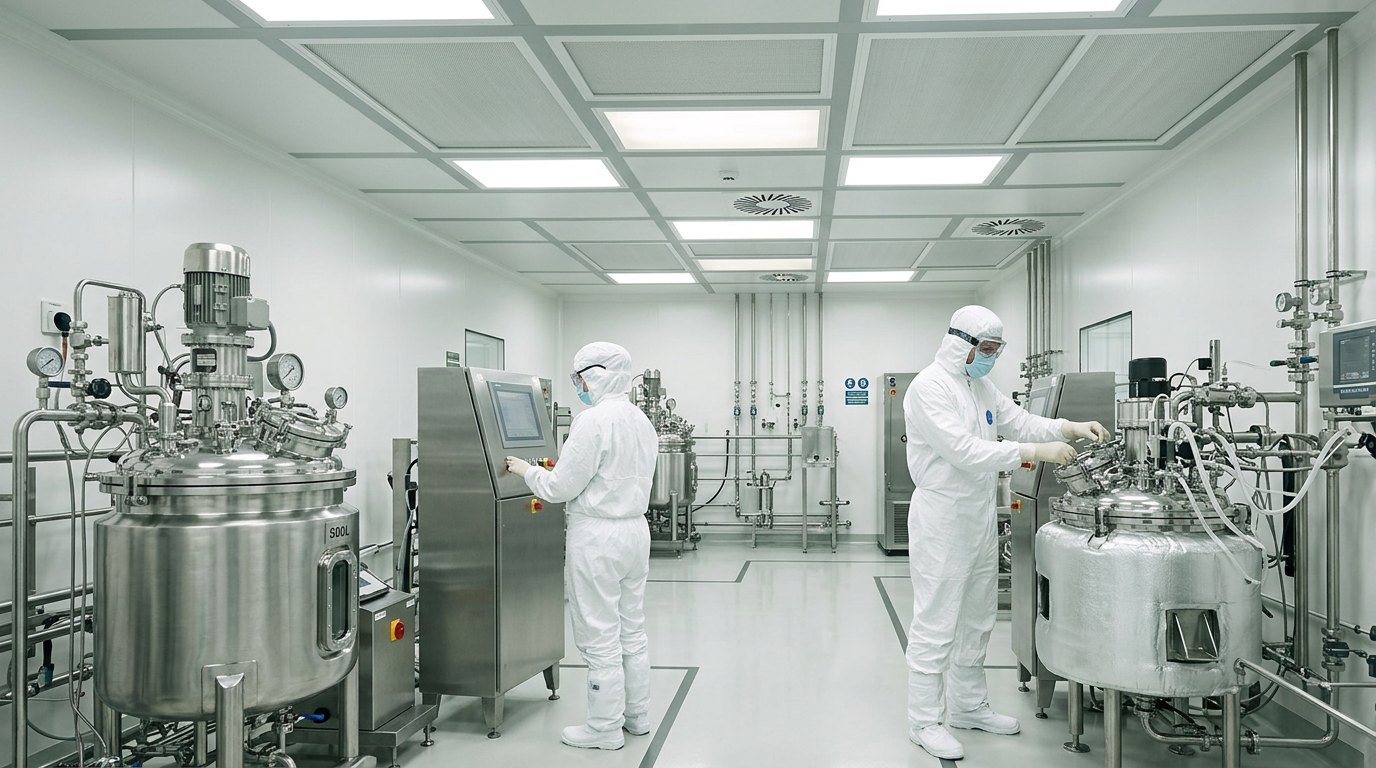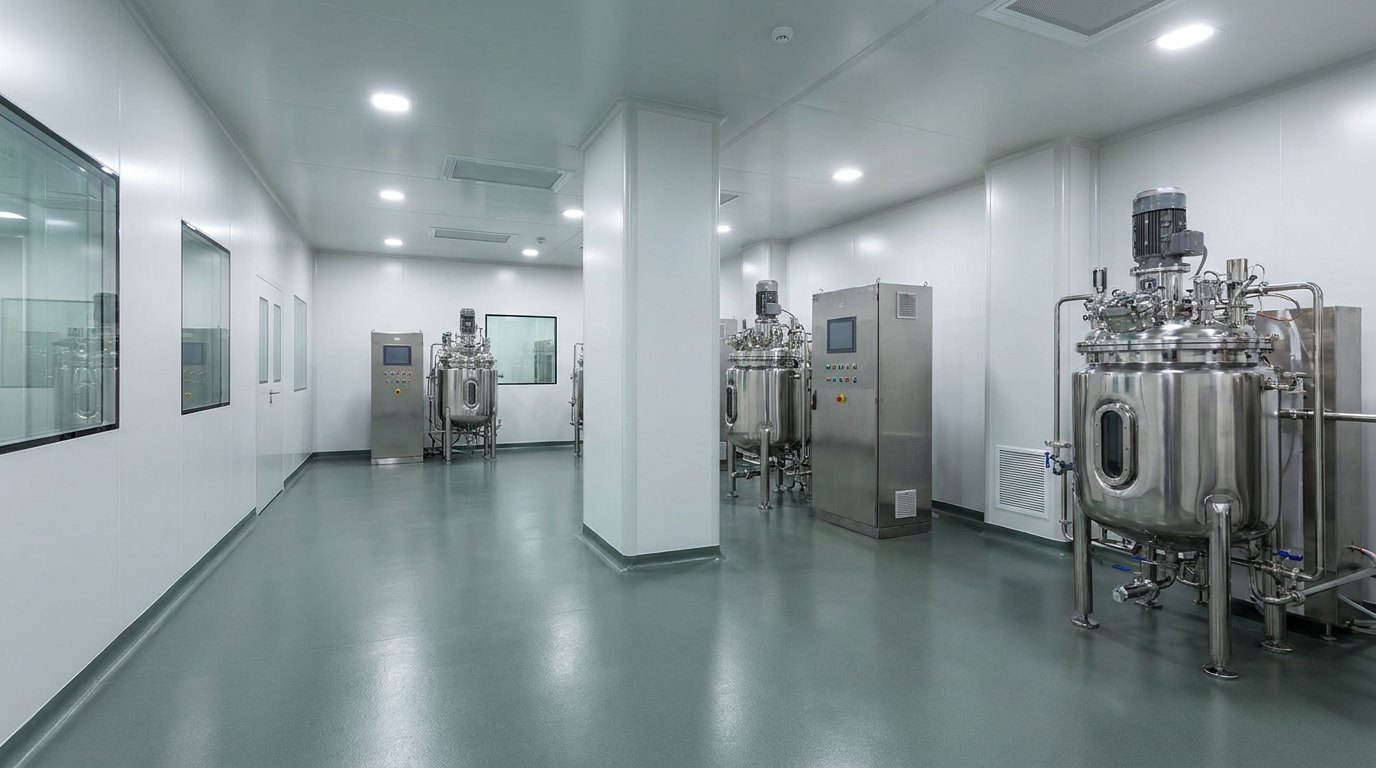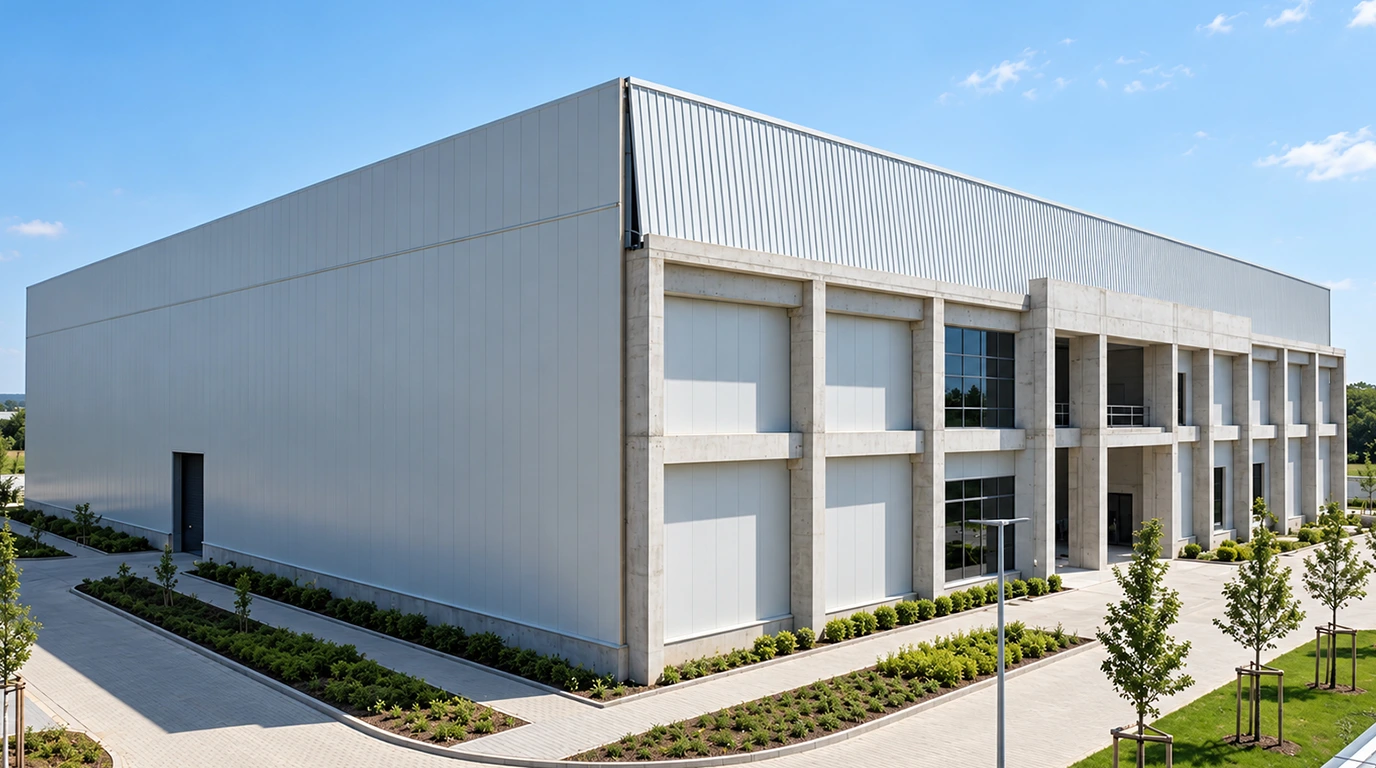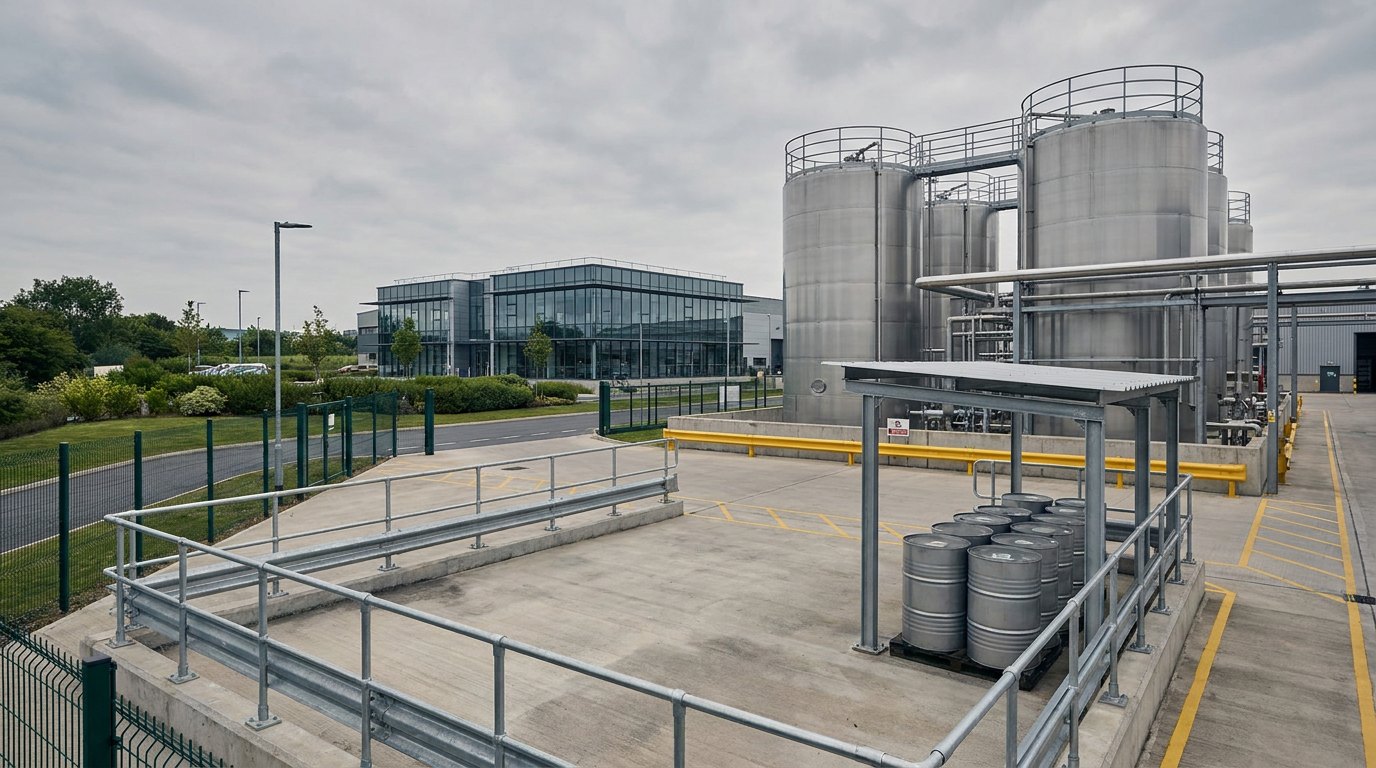
Our flagship integrated campus: 14 blocks, of which 9 are dedicated to API manufacturing through 17 clean room modules, with capability for hydrogenation and cryogenic reactions. The fully automated Metformin HCl block runs on a DCS system with state-of-the-art powder transfer, supported by five purified-water systems, one WFI system and a QC laboratory with the latest instrumentation. The campus also houses a state-of-the-art oral finished dosage facility and operates as a zero liquid discharge site.
USFDA (USA) · PMDA (Japan) · MFDS (Korea) · ANVISA (Brazil) · COFEPRIS (Mexico) · German Health Authority, BGV · NCPHP (Hungary) · WHO-GMP · CDSCO & FDA Maharashtra (India)
Our newest site, currently under construction: two plants with a dedicated purified-water system and a zero-liquid-discharge waste treatment plant, designed for products such as Dextromethorphan HBr with vertical gravity process flow.
Thirteen plants across plots E-7, E-8 and E-9 with two purified-water systems and a waste treatment plant, including dedicated Metformin HCl and Riboflavin Phosphate Sodium plants with vertical gravity process flow.
A dedicated finished dosage facility for oral solid dosage forms, tablets and capsules, and directly compressible (DC) granules, with capacity expanding to 10.00 billion units per annum. All processing areas, corridors, primary packing, dispensing and sampling areas are built to Class 100,000 / Class D / ISO 8 standards with 0.3µ terminal HEPA filters and a dedicated AHU per processing area, with separate personnel and material airlocks and access control for critical areas.
Purified water is generated at 2,000 L/hr through two-pass RO with EDI, and operations run on SAP S/4HANA with Caliber QAMS and LIMS. Accredited by USFDA (USA), NIPN Hungary (EU), WHO-GMP by CDSCO & FDA Maharashtra (India) and ZAZIBONA (Southern Africa).
Every zone is designed to cGMP requirements, from building structure to airflow, for manufacturing, packaging, testing and release. Expand each principle to see how it’s engineered.

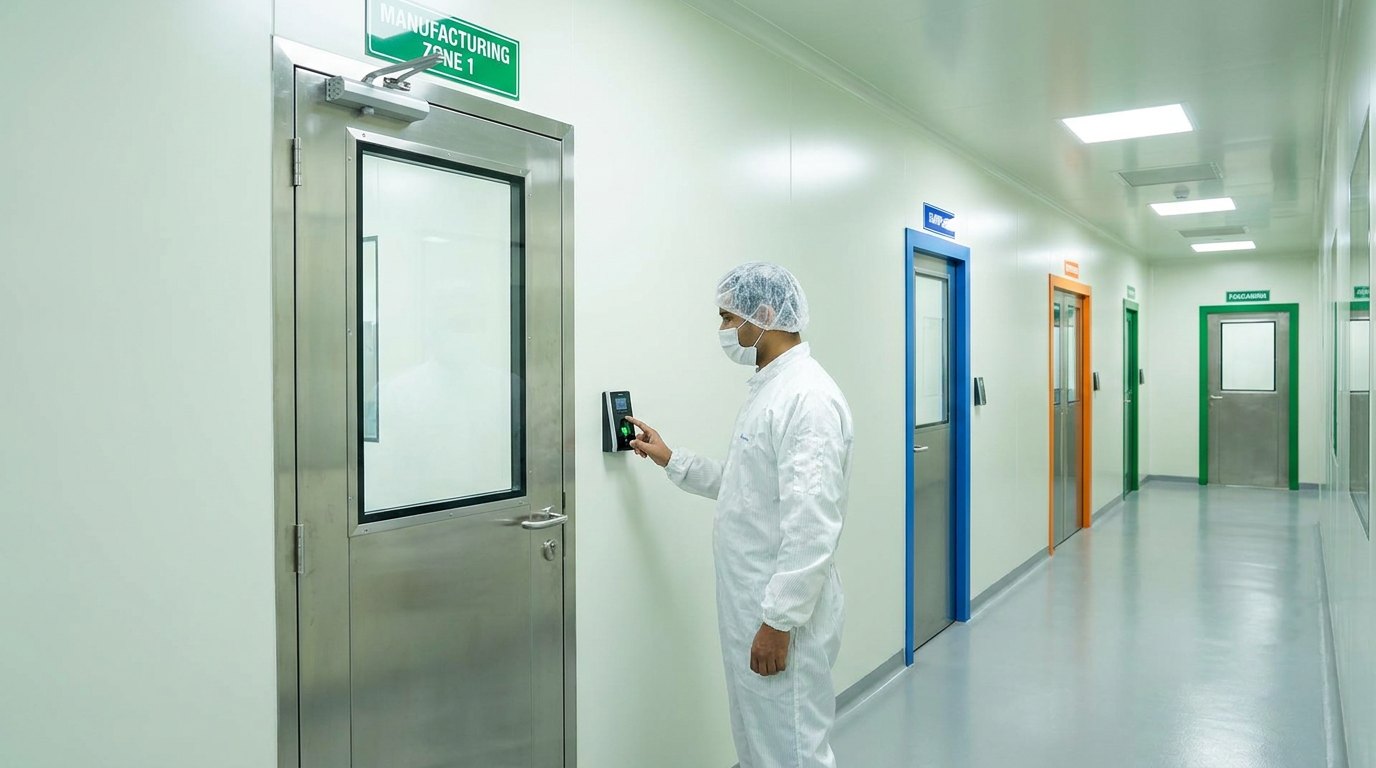
Separate areas for sampling, dispensing, manufacturing, packaging and storage, each with controlled lighting, temperature, humidity, ventilation and drainage. Entry points secured with biometric access control.

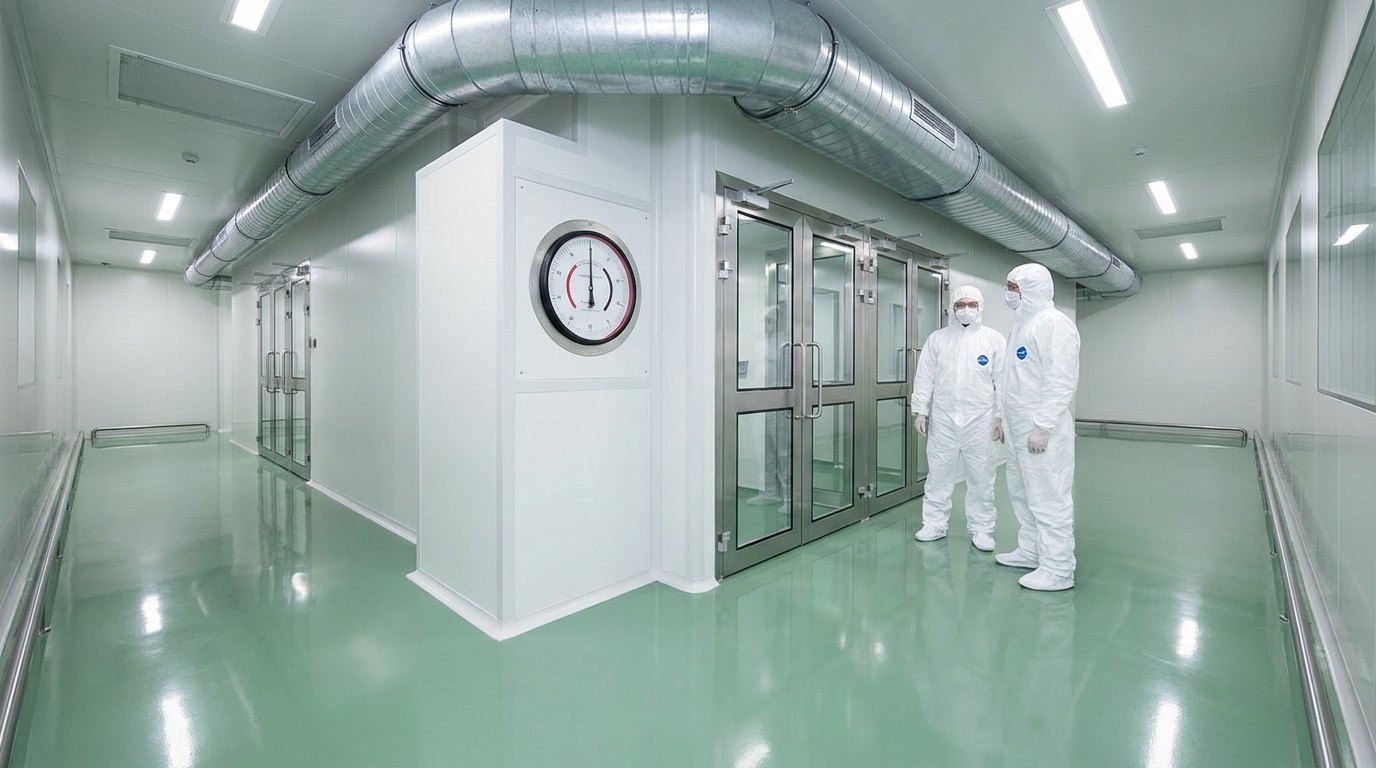
Dedicated HVAC systems maintain ISO 8/Class D and ISO 7/Class C environments with HEPA filtration at 99.995% efficiency and a minimum of 20–35 air changes per hour.

Positive pressure gradients in corridors and dust extraction systems throughout processing areas keep every product stream protected.

Epoxy-coated floors, sealed walls and ceilings, and utility services recessed into surfaces so every finish stays smooth and cleanable.

Every production block is built as a protective shell around its cleanrooms. Constructed to cGMP facility-design standards, the structure excludes moisture, dust and pests, safeguards validated environmental conditions, and protects product integrity from raw material to release.

Solvent operations are managed in a separate, compliant area away from production zones.
Innovating Chemistry for Life – Health, Happiness & Harmony
Copyright © Harman Finochem Ltd. All Rights Reserved.